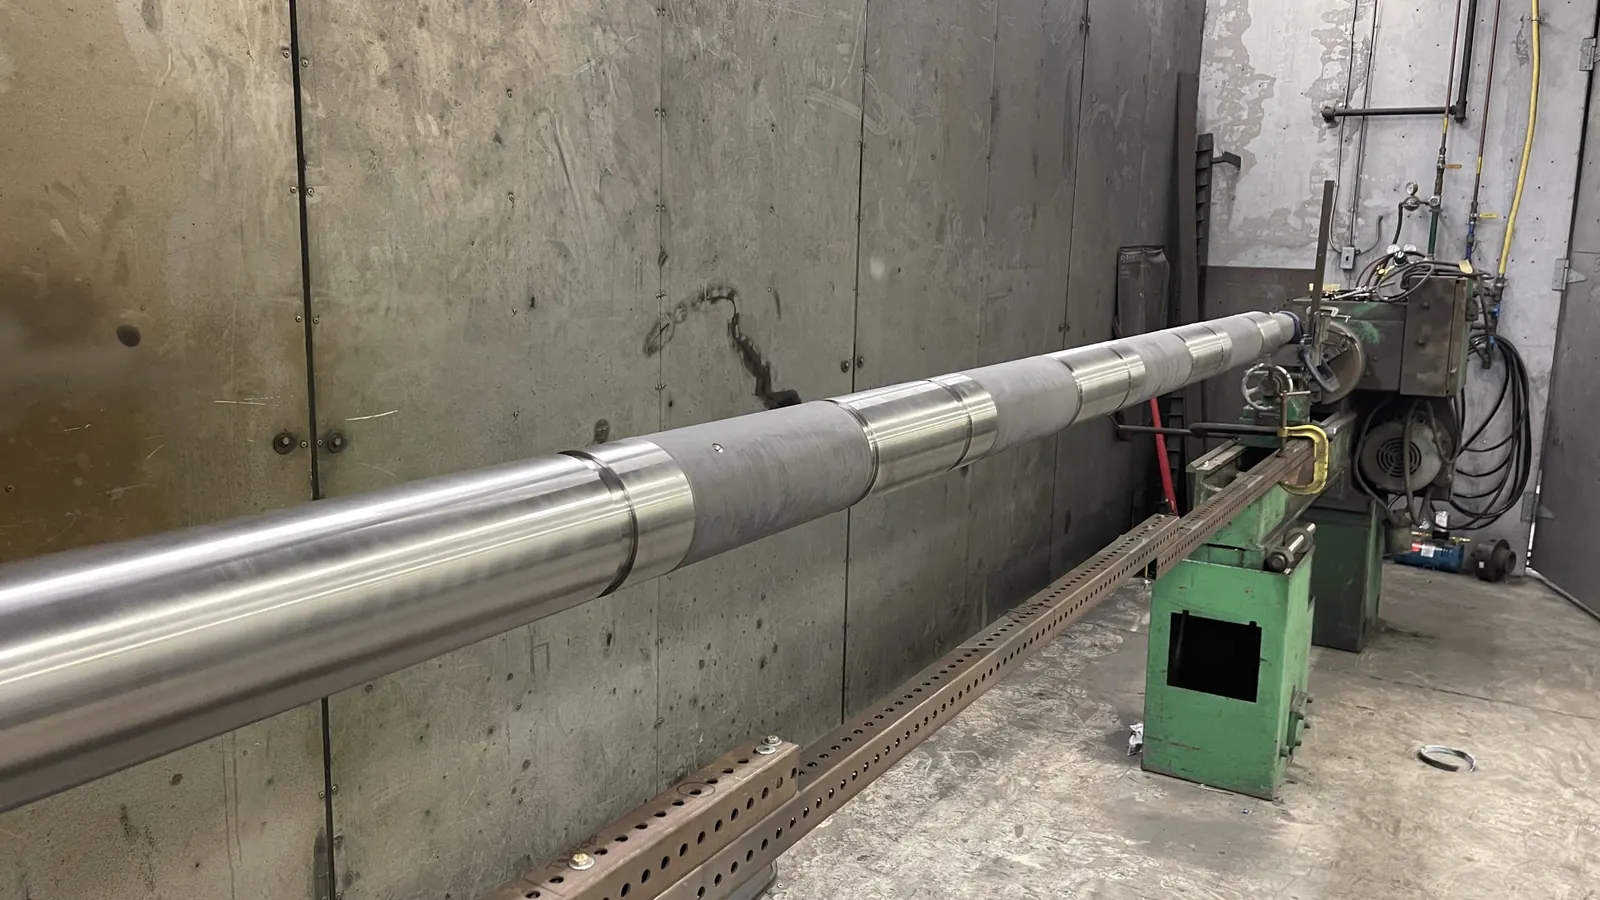
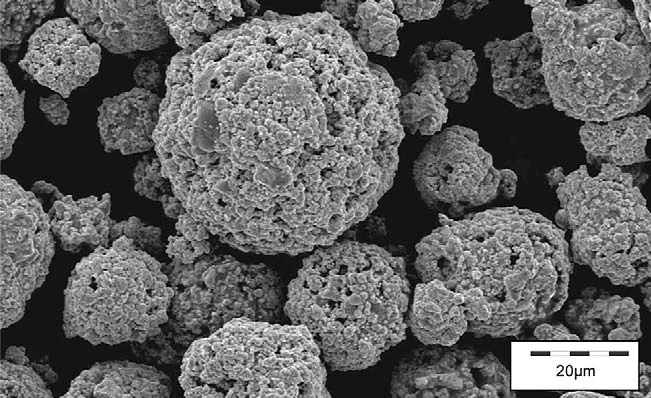
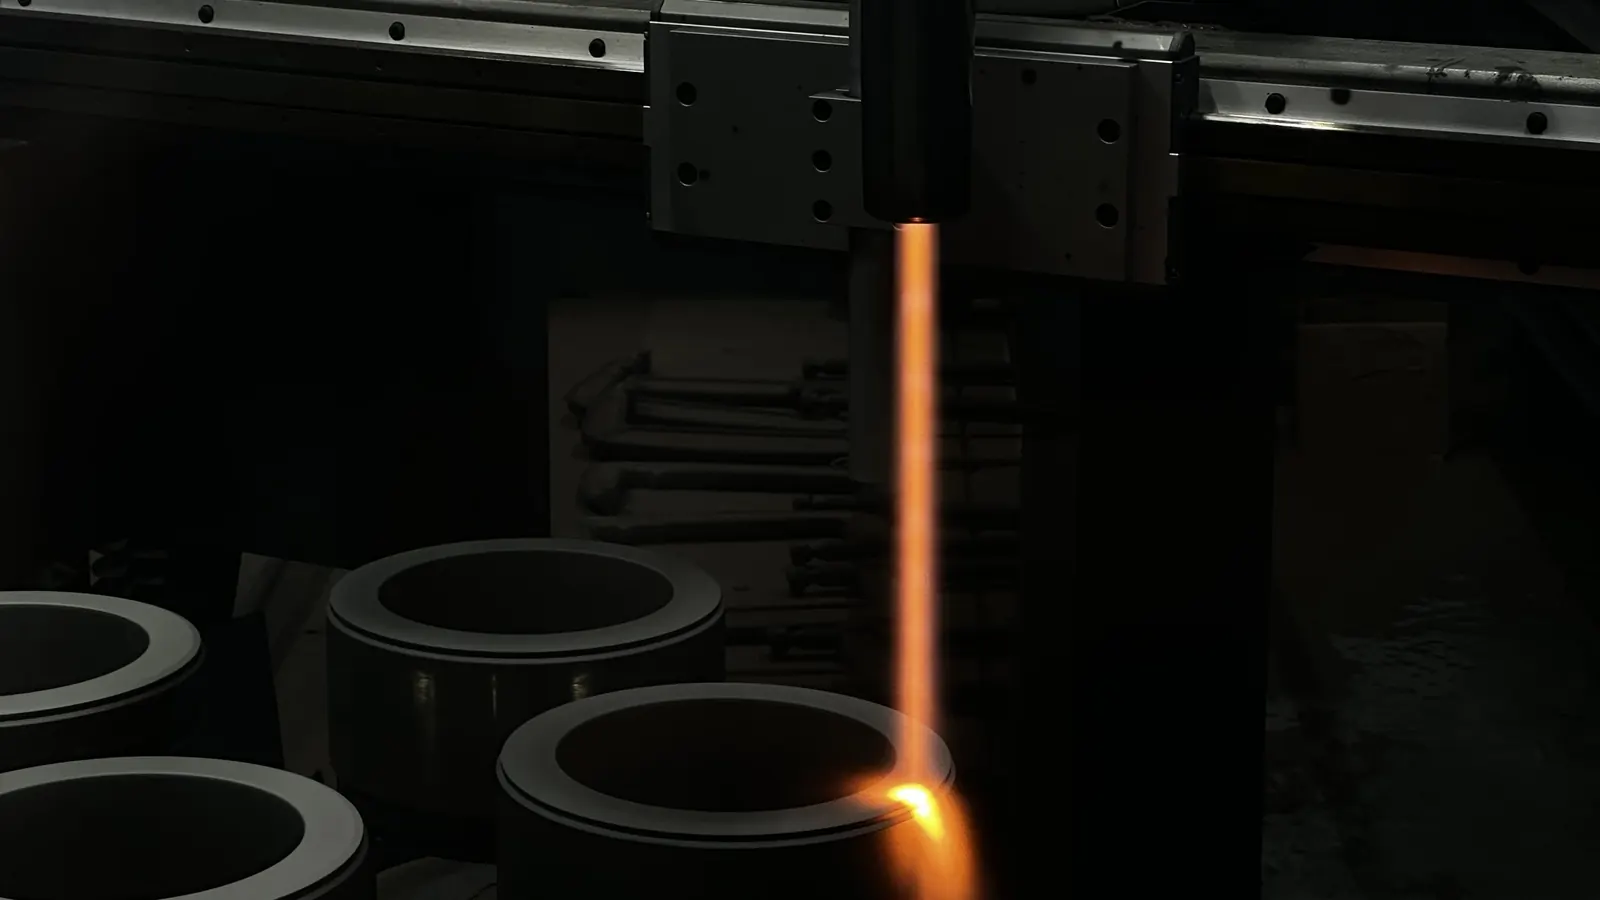
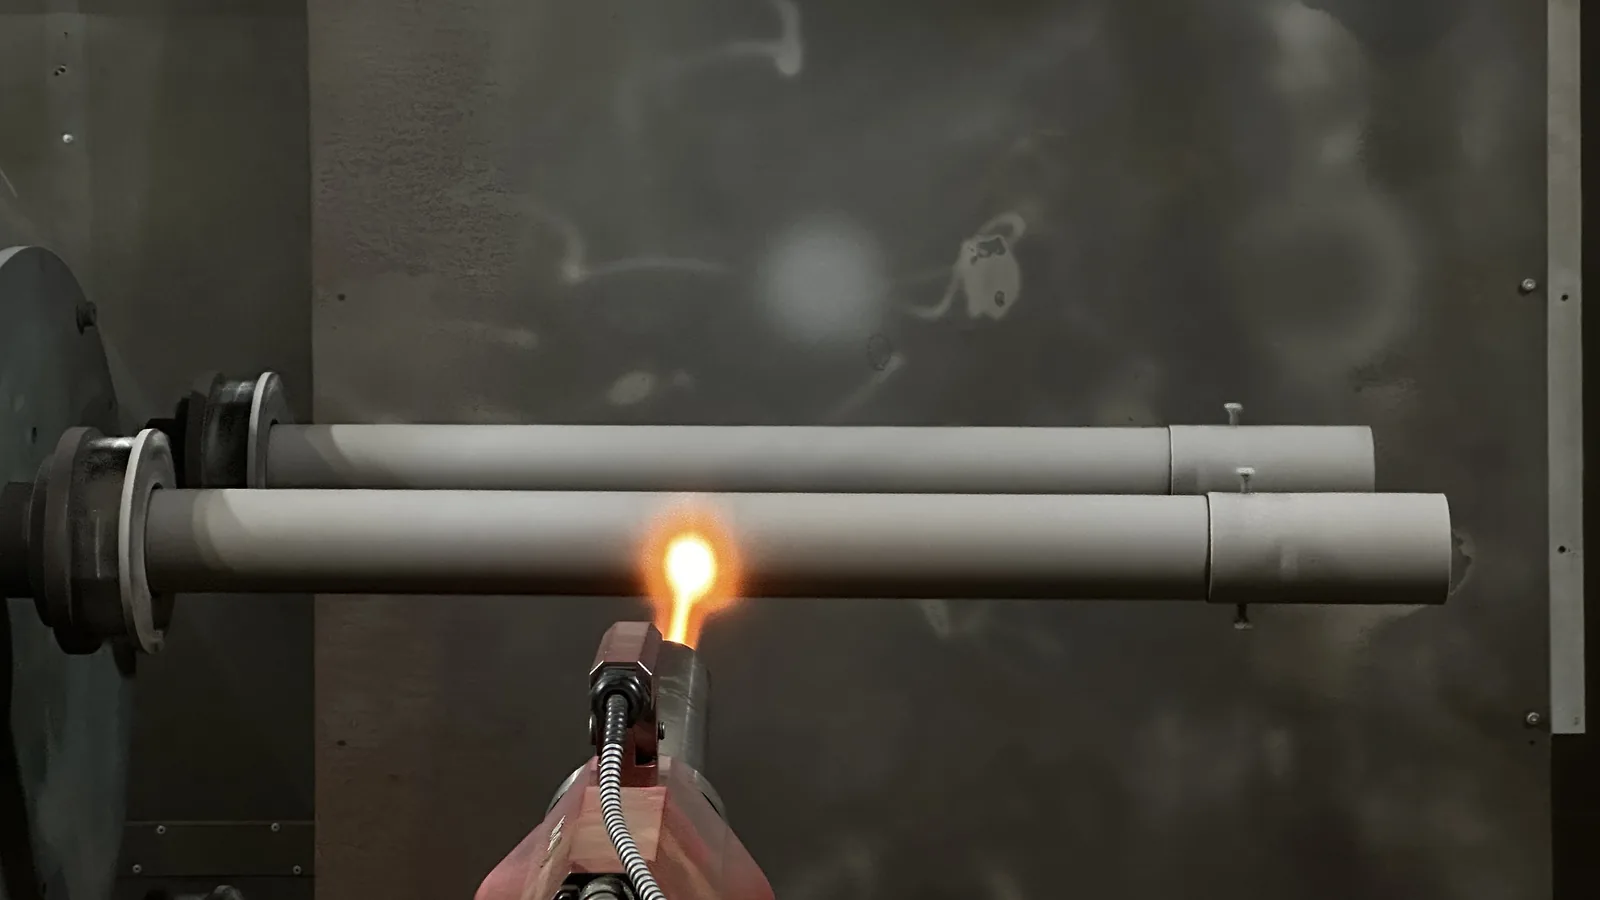
Tungsten carbide coatings are applied with high-velocity processes like HVOF and HVAF, or by plasma spraying. The powder is heated and propelled at high speed onto the part, forming a dense, hard coating, often above 1,200 HV. It offers superior wear resistance and excellent corrosion resistance, significantly extending component life and reducing maintenance costs.
Carbide grades
| Grade | Composition | Hardness | Temperature | Typical use |
|---|---|---|---|---|
| WC-Co | WC in a cobalt binder (typically 6–20% Co) for toughness and adhesion | ~1,000–1,500 HV | Up to ~930 °F (500 °C) | Abrasion and impact; cost-effective and widely used |
| WC-Ni | Nickel binder instead of cobalt | ~900–1,200 HV | Up to ~1,100 °F (600 °C) | Acidic or saline environments |
| WC-Co-Cr | Cobalt and chromium binder (e.g., WC-10Co-4Cr) | ~1,000–1,350 HV | Up to ~1,300 °F (700 °C) | Wear combined with corrosion and oxidation |
| WC-Cr₃C₂-Ni | WC and chromium carbide in a Ni or NiCr binder | 900–1,100 HV (HVOF); 1,200–1,400 HV (HVAF) | — | Wear plus high-temperature and corrosion resistance |
| Cr₃C₂-NiCr | Chromium carbide in a NiCr binder | ~800–1,100 HV | Oxidation resistance to ~1,600 °F (870 °C) | High-temperature, oxidizing service; see chrome carbide |
Tungsten carbide by process
| Process | How it works | Resulting coating |
|---|---|---|
| HVOF | Oxygen and fuel (kerosene, propane or hydrogen) create a supersonic jet; particles reach around 1,000 m/s | Dense and well adhered, porosity <1–2%, 1,000–1,300 HV. Superior wear and moderate corrosion resistance |
| HVAF | Compressed air and fuel (propane or natural gas) give a lower-temperature flame; particles reach 1,000–1,500 m/s | Even denser, porosity <1%, higher bond strength, up to 1,500 HV. Better corrosion resistance from less oxidation |
| Plasma | A plasma arc (argon or nitrogen) up to 30,000 °F melts the powder | Moderate density, 2–5% porosity, 900–1,100 HV. Versatile on complex shapes, but less wear resistant in extreme abrasion |

What we apply
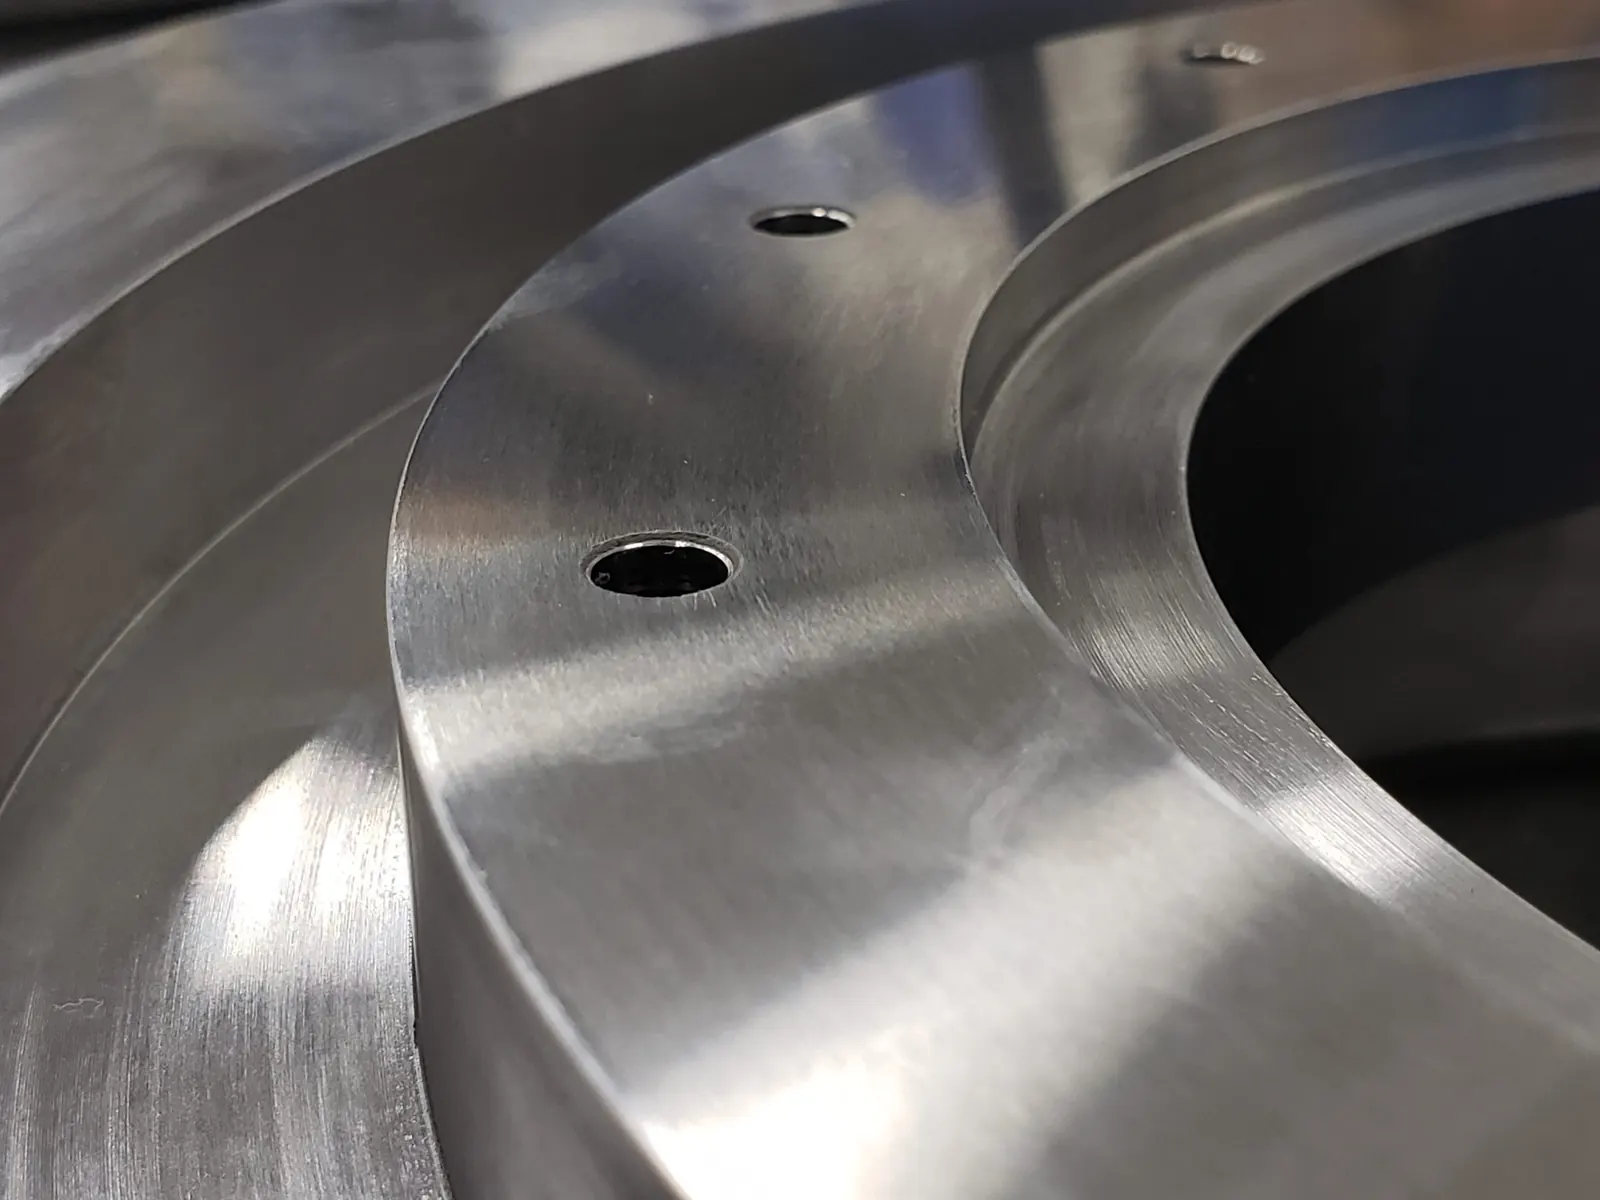
We apply WC-Co, WC-Ni, WC-Co-Cr, WC-CrC-Ni and many more formulations by HVOF, HVAF and plasma in our Allentown shop, then grind and lap them in-house. Carbides can be ground and lapped to an extremely smooth 1 Ra finish.
See how tungsten carbide nearly tripled die life for a wind tower manufacturer.