Thermal spraying is a family of processes in which fine metallic or non-metallic materials (feedstock) are sprayed onto a prepared surface to form a solid coating. The coating adds the surface properties you need, like wear resistance, without changing the core properties of the substrate. For example, titanium wear rings can be given a hard tungsten carbide coating.
What thermal spray coatings do
- Wear resistance: protect rollers, blades and pump components from abrasion and erosion.
- Corrosion protection: shield pipes, valves and structural steel from harsh chemicals and environments.
- Thermal barriers: insulate turbine blades and boiler tubes against high temperatures.
- Electrical insulation: dielectric coatings prevent conductivity in electronics and optics.
- Surface restoration: rebuild worn shafts and bearings and extend their service life.
- Friction control: low-friction or non-stick surfaces for rollers and molds.
See them at work in our case studies.
Why coat instead of replace
Better properties
Coatings extend the life of parts like rollers and valves with superior wear resistance. They add corrosion protection for harsh environments, improve thermal resistance at high temperatures, and can reduce friction in moving parts.
Restore failing parts
Worn and corroded parts that would otherwise be scrapped can be reclaimed with dimensional repair coatings and brought back to specification again and again, yielding considerable savings over time.
Replace industrial hard chrome
Traditional chrome plating uses hexavalent chromium, which faces strict regulation because of health and environmental risks. HVOF, HVAF and plasma coatings offer comparable or superior wear and corrosion resistance without hazardous byproducts, and the powder overspray is typically non-soluble and recyclable. See chrome carbide.
The payoff: less downtime, lower costs and better productivity.
Coating processes
Five processes, all in-house
We run five thermal spray processes in our Allentown shop and apply the coating your drawing calls for, or recommend one if you don’t have a spec yet.
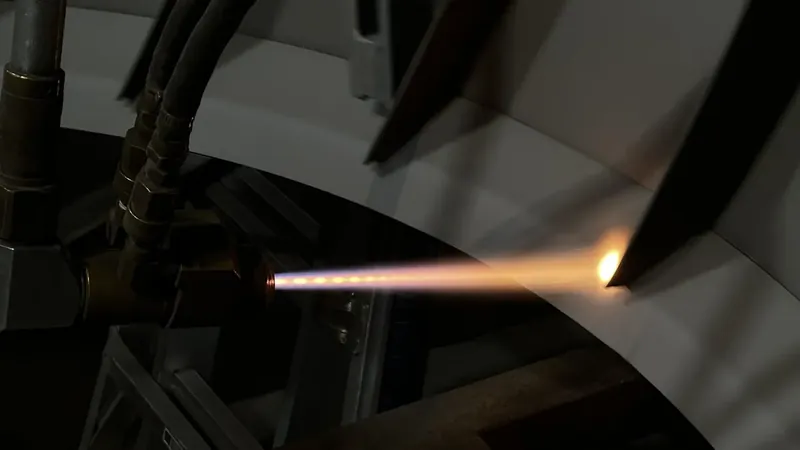
HVOF Coating
Supersonic oxy-fuel spray for dense, well-bonded carbide and alloy coatings that resist wear and corrosion.
Used for
Wear + corrosion
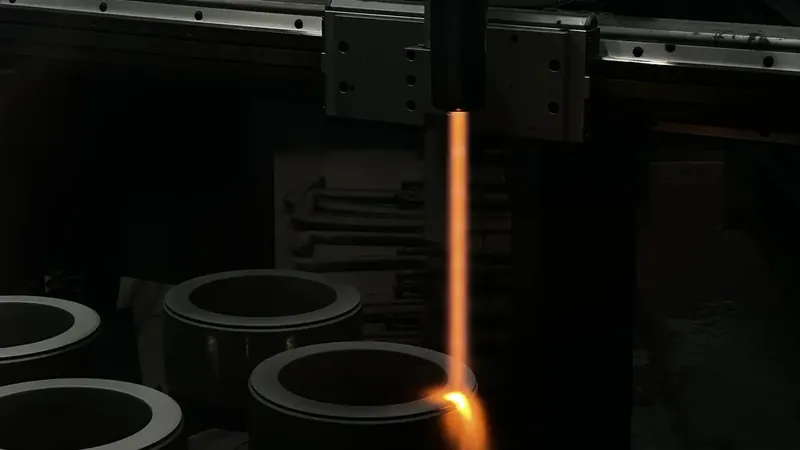
HVAF Coating
Air-fuel spray that keeps carbides cooler, giving harder, near-oxide-free coatings with better impact resistance.
WC hardness
1,250–1,500 HV300
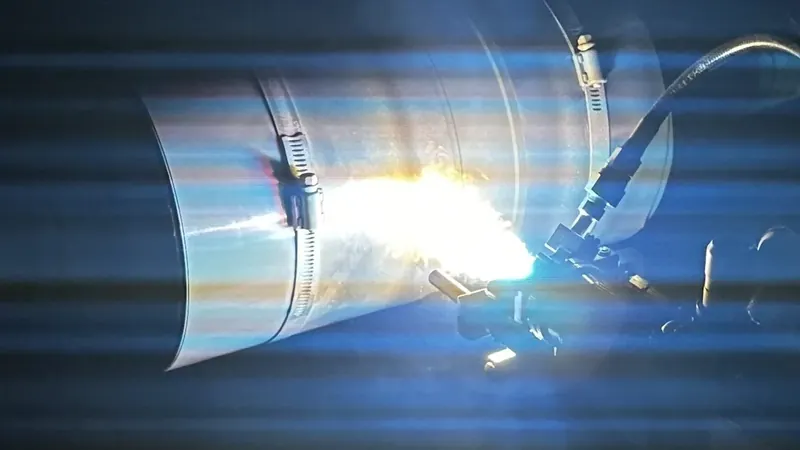
Plasma Spray
High-temperature plasma for chromium oxide, aluminum oxide and other ceramics, plus abradable clearance-control coatings.
Used for
Ceramics & abradables
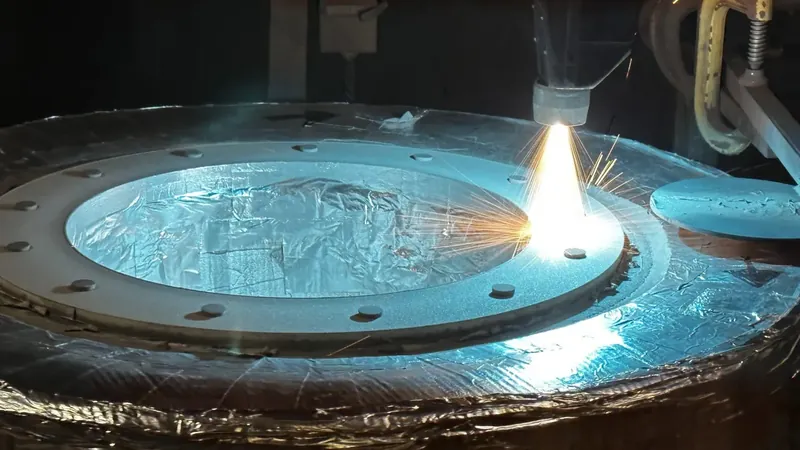
Twin-Wire Arc & Flame
Fast, economical metal build-up for dimensional repair and corrosion protection on large surfaces.
Used for
Repair & build-up
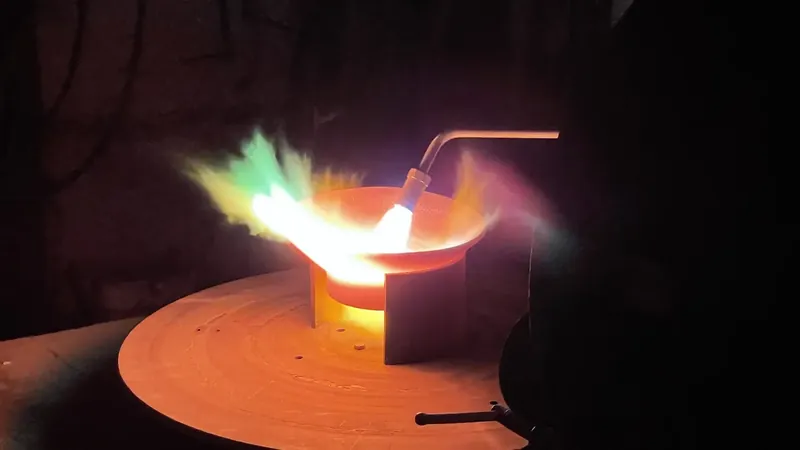
Fused Coatings
Self-fluxing alloys sprayed, then fused at 1,800–2,200 °F into a metallurgical bond that stands up to abrasion, corrosion and impact.
Hardness
50–65 HRC
Have a part to coat?
Send the drawing with your quantity and timeline. Include the coating spec if you have one; if not, we’ll recommend a coating and process.
Comparing the processes
| Process | Heat source | Best known for |
|---|---|---|
| HVOF | Fuel and oxygen combust into a high-speed jet | Dense, durable carbide and alloy coatings with excellent wear and corrosion resistance |
| HVAF | Fuel burned with compressed air: slightly cooler, higher velocity than HVOF | Denser, harder carbide coatings |
| Plasma | Plasma arc from ionized argon or nitrogen, up to 30,000 °F | Oxide ceramics and other high-temperature materials |
| Twin-wire arc | Electric arc between two wires; compressed air sprays the metal | Bond layers, dimensional repair and corrosion protection |
| Fused | Flame-sprayed self-fluxing alloy, then fused at 1,800–2,200 °F (1,000–1,200 °C) | Metallurgically bonded coatings for pump sleeves, rollers and high-impact parts |
Have a part to coat? Send us the drawing or coating spec for a quote.