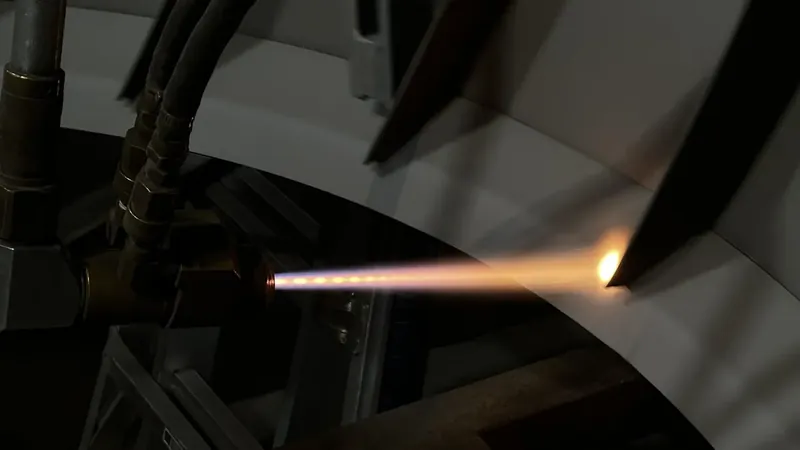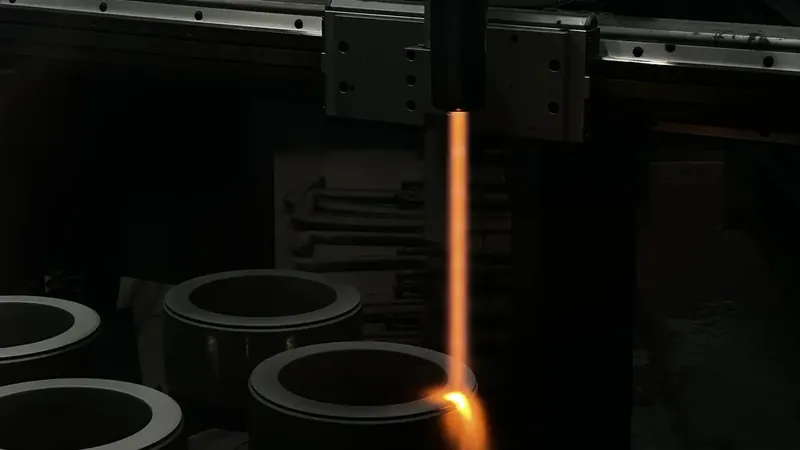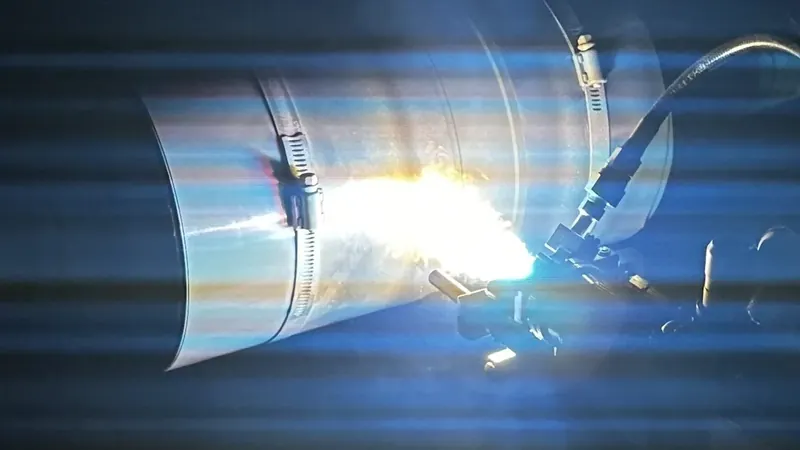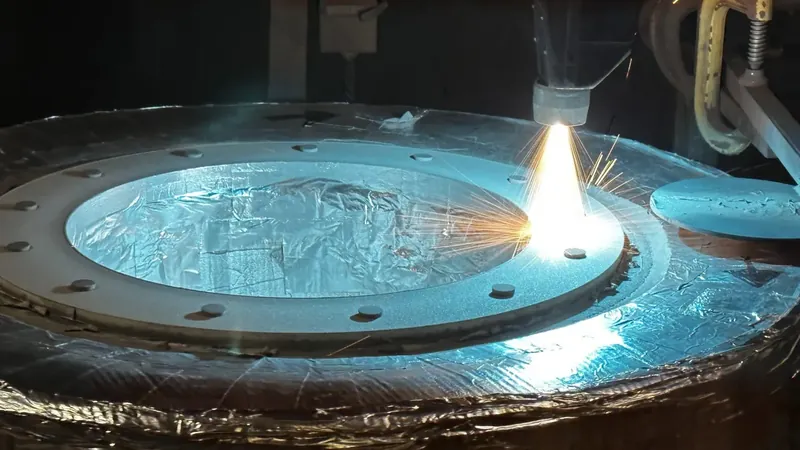
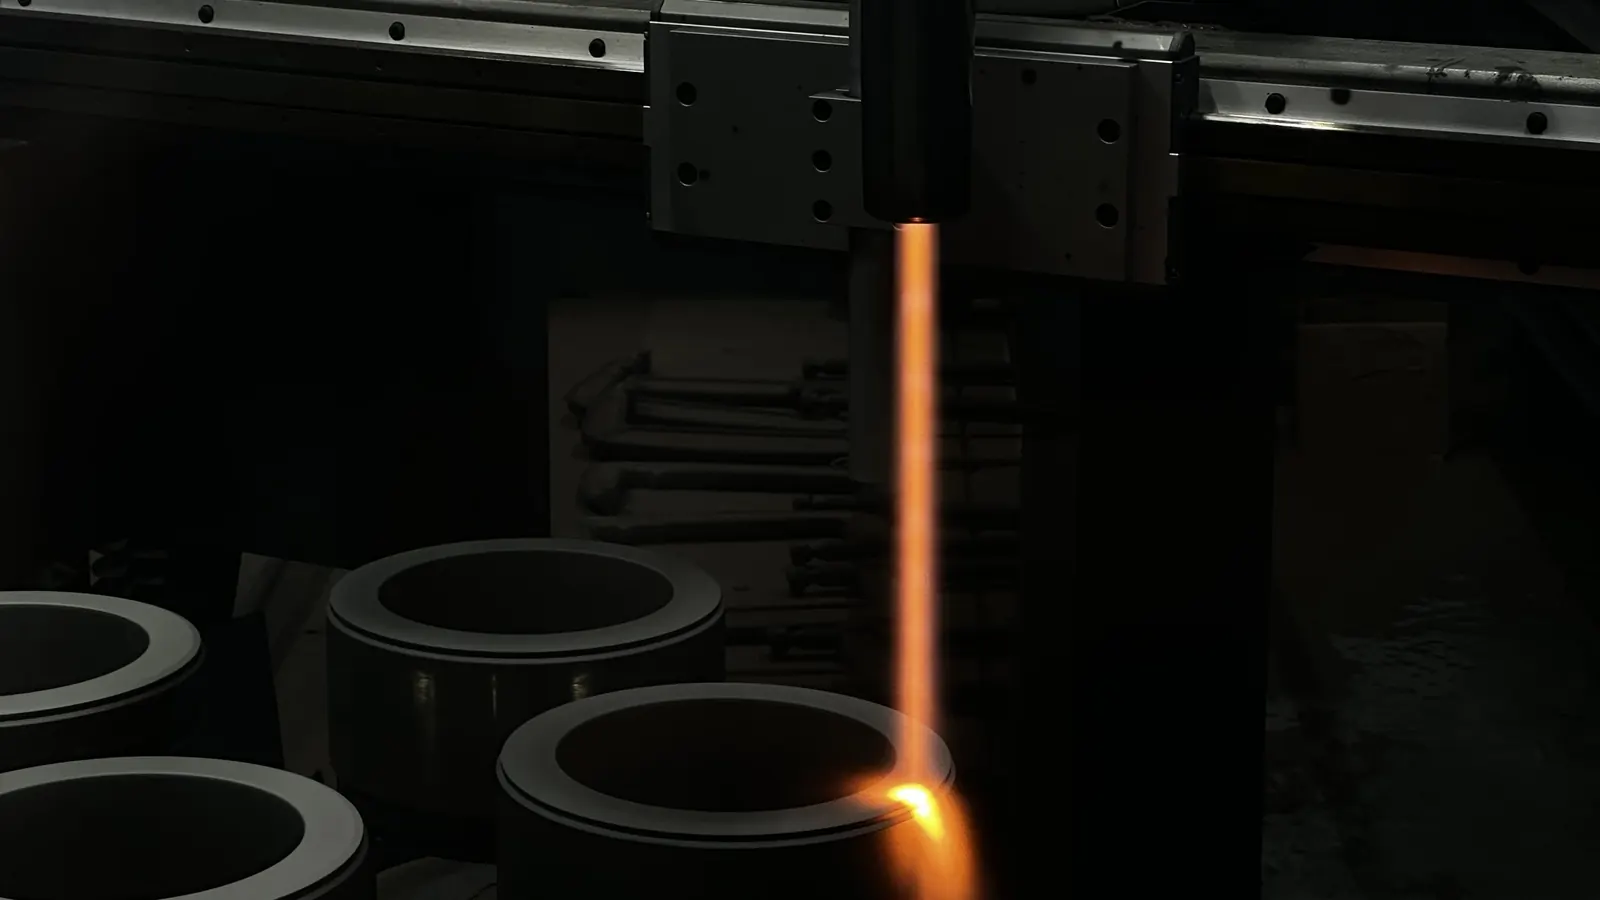
Longevity Coatings has invested in HVAF (high-velocity air-fuel) equipment. It lets us apply carbide coatings with hardness, wear resistance and durability beyond what traditional methods achieve.
HVAF vs. HVOF
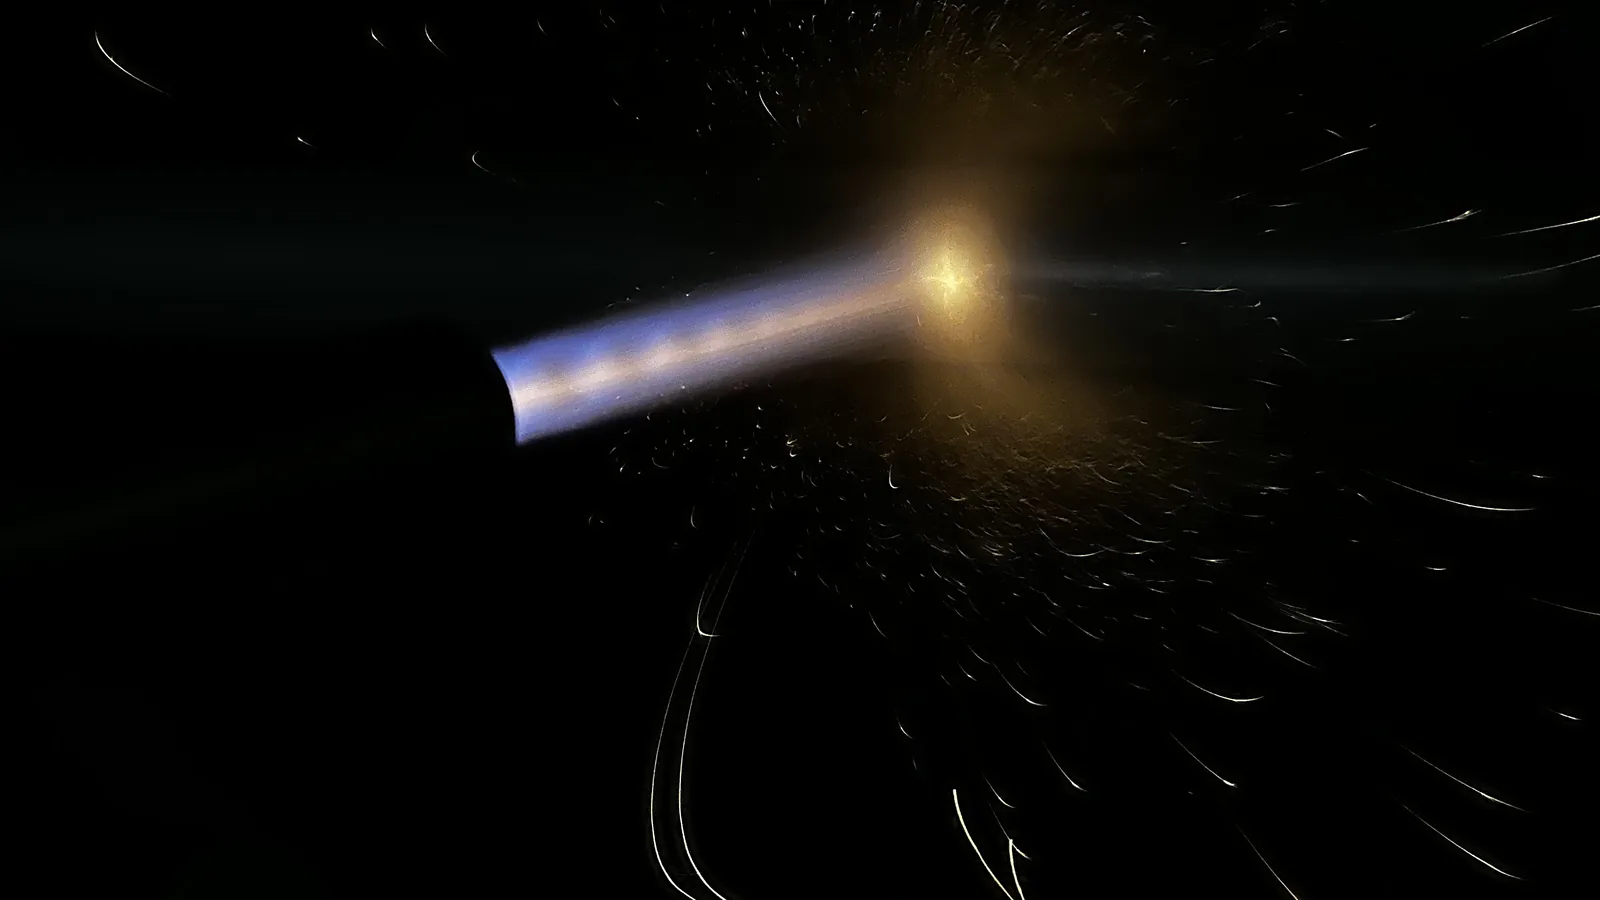
HVAF burns fuel with compressed air instead of the oxygen used in HVOF. The cooler process minimizes oxidation and thermal degradation of the coating material. Coatings come out denser and smoother, with better corrosion and wear resistance, excellent bond strength and lower porosity.
It is also more economical: it uses less fuel and can apply thinner, high-quality layers. Carbide coatings of 0.010–0.050″ are typical. Very fine feedstock can produce smooth, hard coatings, as-sprayed or lightly polished, with surface finishes as fine as 50 Ra.
| HVAF | HVOF | |
|---|---|---|
| Oxidizer | Compressed air | Oxygen |
| Tungsten carbide hardness | 1,250–1,500 HV300 | 1,000–1,300 HV300 |
| Oxygen in the coating | Virtually eliminated | Typically 2–4% as glassy phases |
| Effect on carbide | Lower temperature preserves hardness and crystal structure | Higher flame temperature can form softer phases (W₂C, binder enrichment) |
Why it matters for carbide coatings
HVAF’s lower operating temperature minimizes oxidation and decarburization of tungsten carbide particles during spraying. The flame consumes nearly all available oxygen, so the coating is virtually oxide-free. That has a dramatic effect on a carbide coating’s ability to withstand impact and flexure.
The result is superior wear and abrasion resistance. It is especially valuable for parts like oilfield components, where maximum hardness translates directly into longer service life.
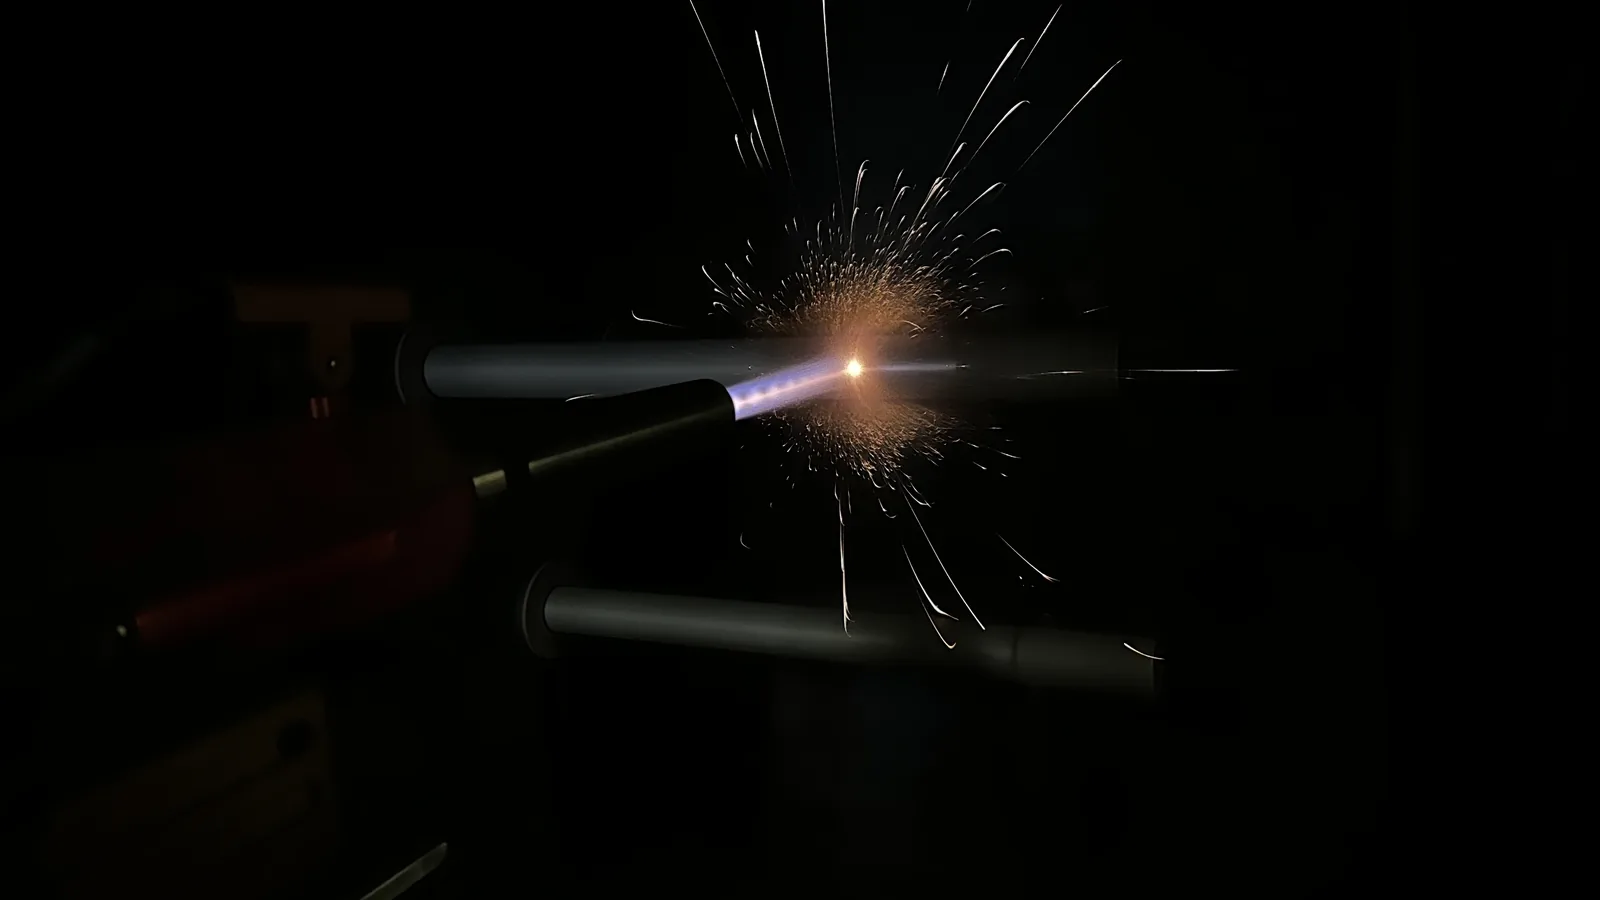
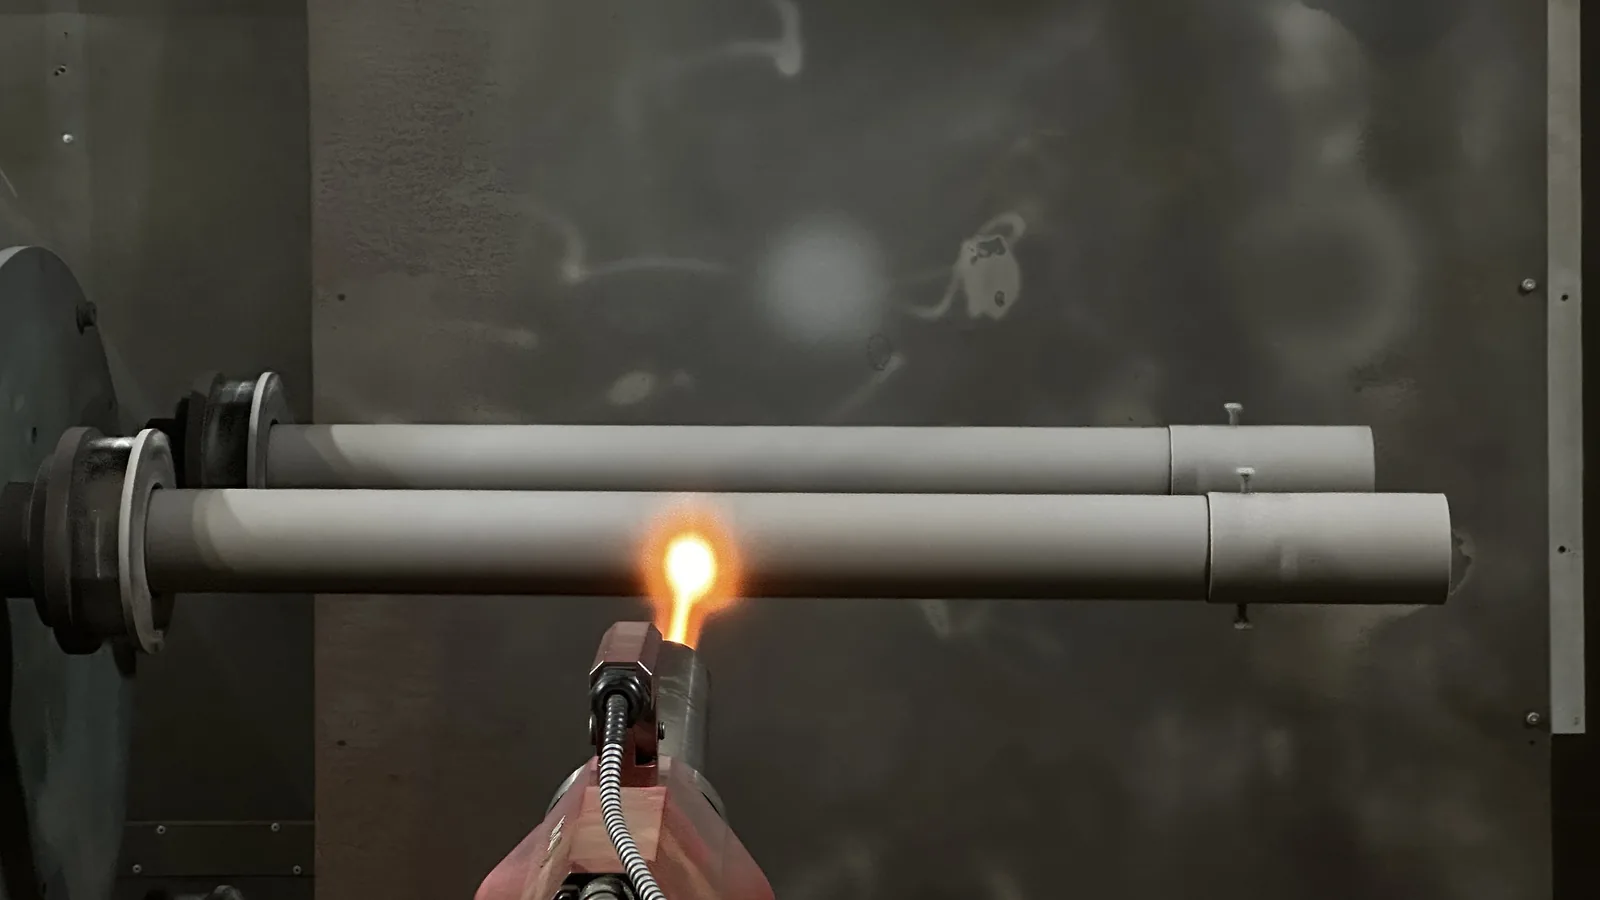
Typical HVAF materials
- Tungsten carbide: WC-Co, WC-Ni and WC-Co-Cr.
- WC-Cr₃C₂-Ni: 1,200–1,400 HV with HVAF, compared with 900–1,100 HV with HVOF.
- Chrome carbide: an alternative to hard chrome plating.
- Metals and alloys: nickel- and cobalt-based alloys and stainless steels.
Finished in-house
HVAF coatings are diamond ground, diamond lapped or diamond super finished to your specifications in our own Allentown machining and finishing shop.