2–3× life
Oil & gas · Wellhead valves
Valve seats & slab gates
Tungsten carbide coated and lapped flat to 12 millionths of an inch, with finishes finer than 1 Ra. The parts outlast those from competing coaters and the OEM.
Mon–Fri 7:00 am – 3:30 pm
6047 Adams Ln, Allentown, PA 18109
HVOF coating in our Allentown shop
Allentown, PA · Lehigh Valley
HVOF, HVAF, plasma and twin-wire arc coatings, plus in-house CNC machining, diamond grinding and lapping. Send us a drawing and get back a finished, coated part.
HVOF & HVAF
Plus plasma, twin-wire arc and fused coatings
Carbides & ceramics
Tungsten carbide, chrome carbide, chromium oxide and more
Spray to finish
Coated, ground and lapped under one roof
Since 2005
Thermal spray in Allentown, PA
Coating processes
We run five thermal spray processes in our Allentown shop and apply the coating your drawing calls for, or recommend one if you don’t have a spec yet.
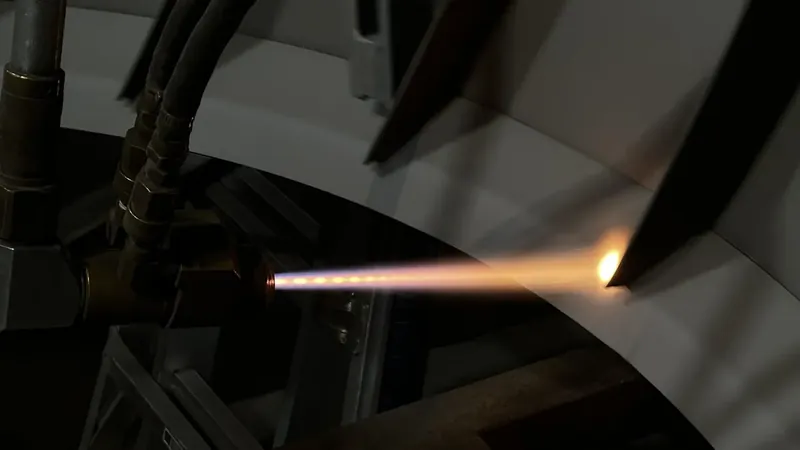
Supersonic oxy-fuel spray for dense, well-bonded carbide and alloy coatings that resist wear and corrosion.
Used for
Wear + corrosion
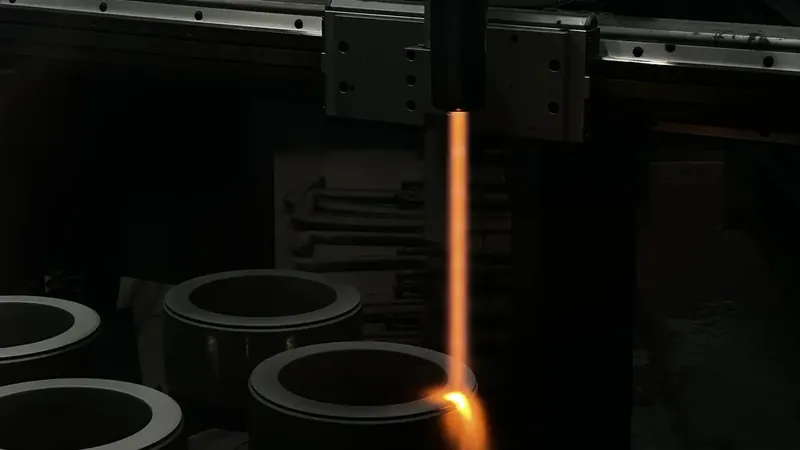
Air-fuel spray that keeps carbides cooler, giving harder, near-oxide-free coatings with better impact resistance.
WC hardness
1,250–1,500 HV300
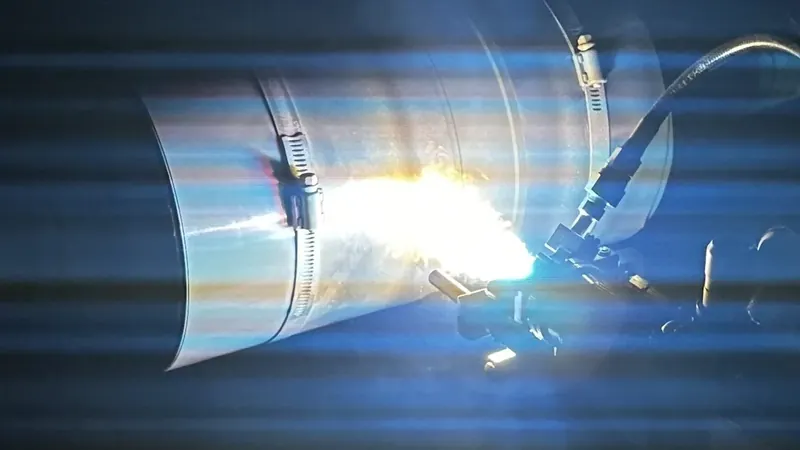
High-temperature plasma for chromium oxide, aluminum oxide and other ceramics, plus abradable clearance-control coatings.
Used for
Ceramics & abradables
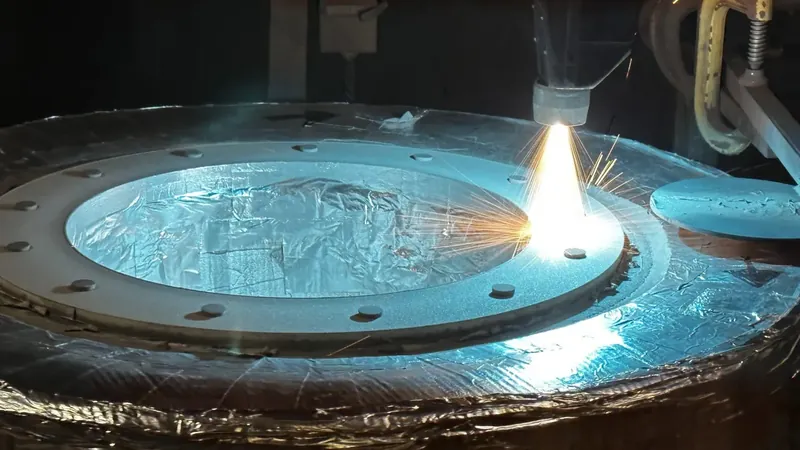
Fast, economical metal build-up for dimensional repair and corrosion protection on large surfaces.
Used for
Repair & build-up
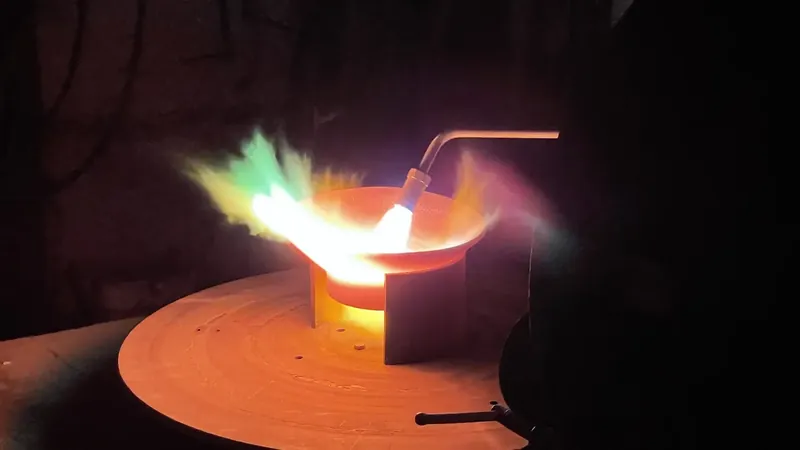
Self-fluxing alloys sprayed, then fused at 1,800–2,200 °F into a metallurgical bond that stands up to abrasion, corrosion and impact.
Hardness
50–65 HRC
Send the drawing with your quantity and timeline. Include the coating spec if you have one; if not, we’ll recommend a coating and process.
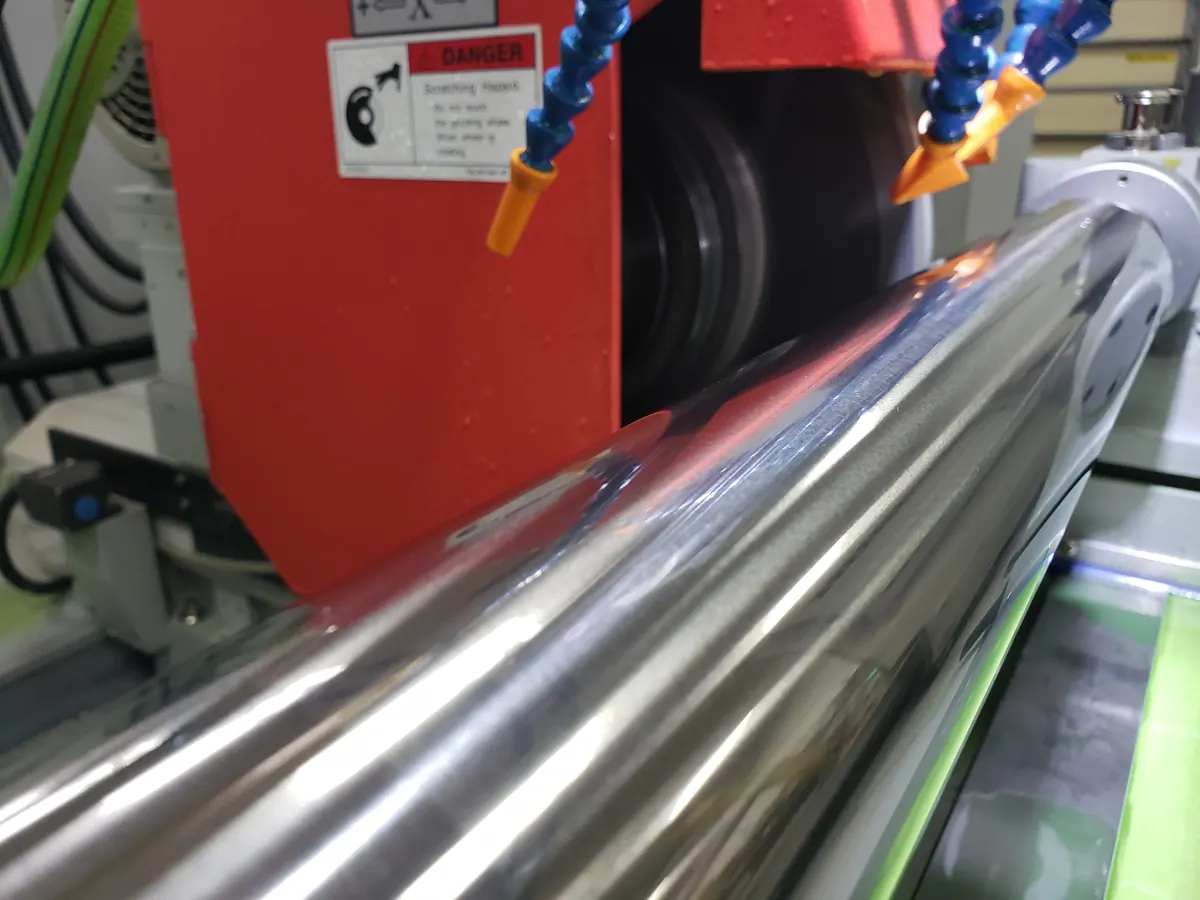
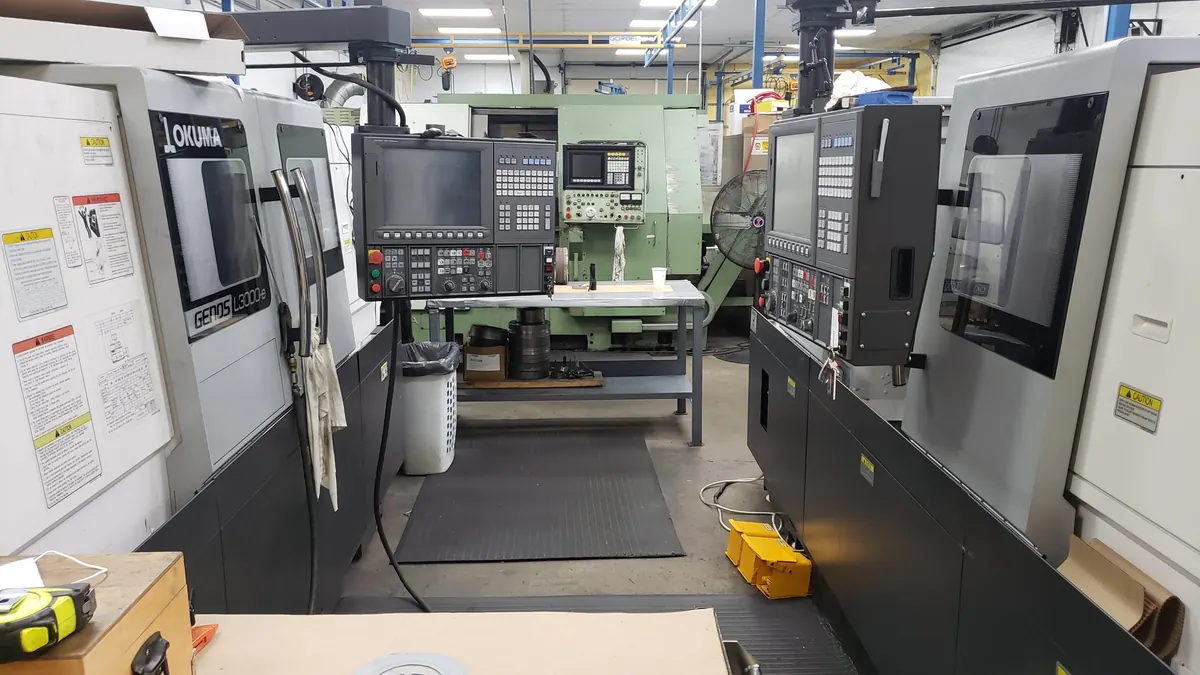
Machining & finishing
We make the part, coat it, and grind or lap it to final size. You deal with one shop and one lead time, with no shipping between vendors.
Results
A few examples of what our coating and finishing work has done for customers’ parts.
2–3× life
Oil & gas · Wellhead valves
Tungsten carbide coated and lapped flat to 12 millionths of an inch, with finishes finer than 1 Ra. The parts outlast those from competing coaters and the OEM.
7k → 20k cycles
Wind energy · Tube-flaring dies
A tungsten carbide coating nearly tripled die life for NRG Systems. It also let them build the dies from a less expensive grade of steel.
100% of the line coated
Battery manufacturing
We ceramic-coated the dryer vessel, valves, hoppers and agitators. That added extreme wear resistance without contaminating the battery chemistry.
Coating materials
Carbides, oxide ceramics, metal alloys, abradables and many more, applied to your drawing or specification.
Industries
From downhole tools to paper machine rolls, we coat the components that keep production running.
Gate valves & seats, chokes, downhole tools
Turbine blades, rotors, steam valve parts
Paper machine, calender & suction rolls
Anilox, impression, dryer & chill rolls
Pumps, agitators, screws & extruders
Crusher parts, conveyor rollers, chutes
Impellers, centrifuges, seals & shafts
Pump rotors, shaft sleeves, control valves
Scrubber parts, cyclone separators
Hydraulic rods, crusher & mixer parts
How it works
Upload a print, photo or spec sheet with your quantity and timeline.
We review your drawing and spec, or recommend a coating and process, then send a quote.
Machining, spraying, grinding and lapping, all done in-house.
Finished parts go out from our dock, ready to install.
About Longevity
Founder Mark Purington managed his father’s thermal spray plant while still a student at Penn State. He started Longevity Coatings in 2005, and we moved to our current two-acre site near Lehigh Valley International Airport in 2007.
Our quality management system conforms to ISO 9001:2015.
Request a quote
Attach your drawing, and the coating spec if you have one. No spec yet? Tell us how the part is used and we’ll recommend a coating and process with the quote.